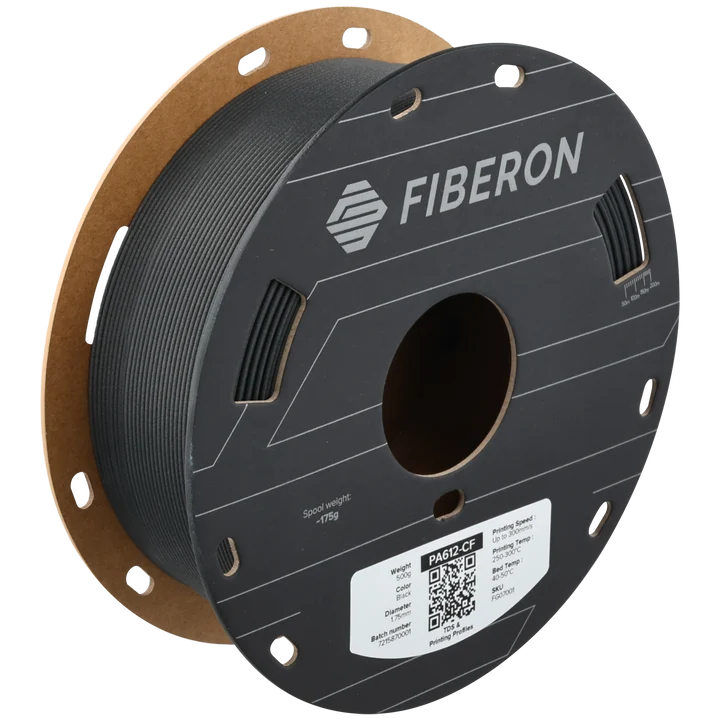
Fiberon™ PA612-CF15
Fiberon™ PA612-CF15 is a 15% carbon fiber-reinforced long-chain nylon filament combining low moisture absorption with high structural rigidity.Formulated with Warp-Free™ technology, it delivers superior dimensional accuracy, elevated heat resistance, and reliable printability for demanding engineering applications
Volume Pricing Available
Polymaker’s Fiberon™ PA612-CF15 bridges the gap between traditional PA6 and PA12 polymers by using a long-chain copolyamide matrix reinforced with 15% carbon fiber loading by weight.This specialized chemical structure offers significantly lower humidity sensitivity than PA6-based composites while retaining higher mechanical strength and modulus than PA12 variants.
Featuring a tensile strength of 91.9 MPa and a bending strength of 138 MPa in the XY orientation, this material provides industrial-grade structural performance.Integrated with proprietary Warp-Free™ crystallization control technology, PA612-CF15 minimizes thermal shrinkage during builds, ensuring extreme dimensional fidelity and high inter-layer strength across complex components.
Key Benefits
15% short carbon fiber fill for high stiffness and reduced component weight
Superior moisture resistance compared to standard PA6 and PA6/66 formulas
Engineered with Warp-Free™ technology for minimal distortion on large builds
High thermal resistance with HDT reaching up to 175.1°C @ 0.45 MPa
Outperforms PA12 composites in mechanical strength and flexural modulus
Clean matte black surface finish that masks build lines effectively
Excellent inter-layer adhesion for isotropic load distribution
High-speed motion compatibility up to 300 mm/s
Stable dimensional accuracy for precision mechanical assemblies
Consistent extrusion reliability across standard and enclosed FDM platforms
Typical Applications
Custom end-of-arm robotic tooling and structural grippers
Industrial manufacturing aids, assembly jigs, and alignment fixtures
High-stress automotive mounts, brackets, and under-hood housings
Aerospace and drone structural frames, arms, and motor mounts
Precision electronic enclosures and protective housings
Replacement metal structural stock in lightweight assemblies
End-use functional hardware exposed to humid environments
Thermal-resistant prototype components operating under mechanical loads
Mechanical linkages, levers, and load-bearing brackets
Fiberon™ PA612-CF15 is particularly well suited for structural applications where low moisture sensitivity, high mechanical stiffness, thermal resilience, and dimensional precision are required.
Specifications
Material: PA612 Nylon with 15% Carbon Fiber
Filament Diameter: 1.75mm
Available Weights: 0.5kg, 3kg
Available Colors: Black
Density: 1.03 g/cm³
Nozzle Temperature: 250–300°C
Build Plate Temperature: 25–50°C (Do not exceed 50°C)
Maximum Print Speed: Up to 300 mm/s
Cooling Fan: OFF (0%)
Enclosure: Recommended
Nozzle: 0.4mm or larger hardened steel or ruby nozzle required
Drying: 100°C for 10 hours before printing
Mechanical Properties
Tensile Strength XY: 91.9 MPa
Tensile Strength Z: 48.3 MPa
Elongation at Break XY: 2.6%
Elongation at Break Z: 2.1%
Bending Strength XY: 138.0 MPa
Bending Strength Z: 73.5 MPa
Bending Modulus XY: 4583.0 MPa
Young's Modulus XY: 5136.0 MPa
Young's Modulus Z: 2786.0 MPa
Charpy Notched XY: 8.1 kJ/m²
Charpy Unnotched Z: 12.6 kJ/m²
Thermal Properties
Melting Temperature: 210.0°C
Vicat Softening Temperature: 206.0°C
HDT @ 0.45 MPa: 175.1°C
HDT @ 1.8 MPa: 114.3°C
Recommended Print Settings
Nozzle: 250–300°C
Build Plate: 25–50°C (Keep ambient/bed below 50°C to avoid warping)
Print Speed: 30–300 mm/s
Cooling Fan: OFF (0%)
Retraction Distance: 3mm (Direct Drive) / 6mm (Bowden)
Retraction Speed: 40 mm/s (Direct Drive) / 60 mm/s (Bowden)
Drying: 100°C for 10 hours prior to printing
Nozzle: Hardened steel or ruby, 0.4mm or larger
Enclosure: Recommended for temperature stability (print at room temperature ambient)
Due to the abrasive nature of carbon fiber additives, a hardened wear-resistant nozzle is mandatory. To achieve full heat resistance and maximum mechanical strength, post-print annealing at 100°C for 16 hours is recommended.